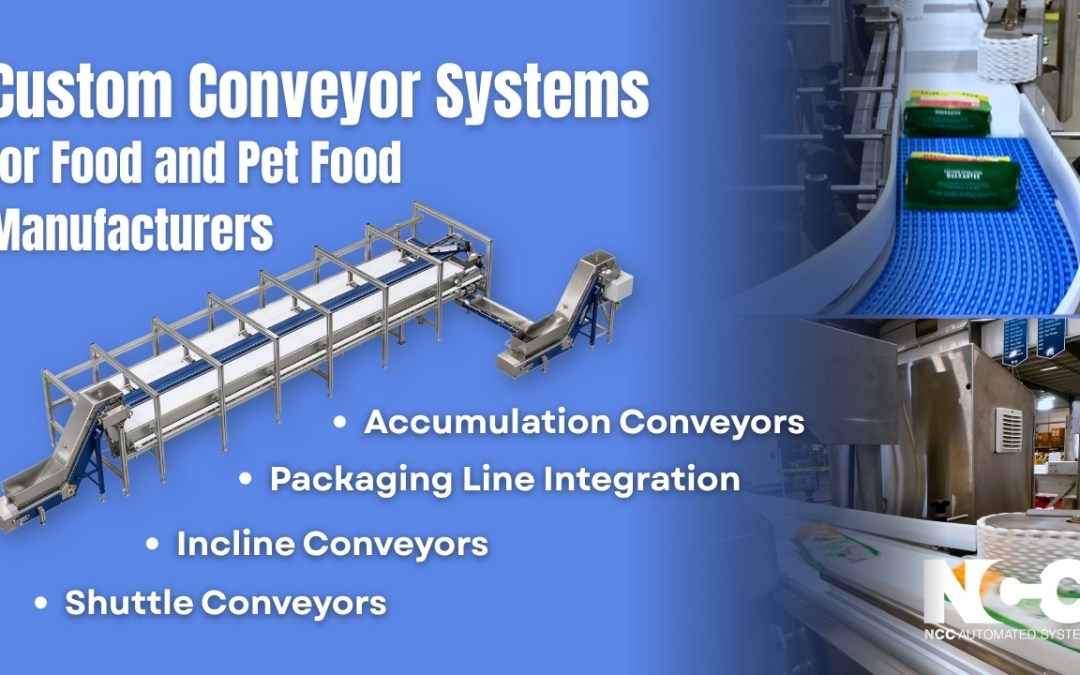
Optimize your production throughput and maintain rigorous sanitary standards with custom conveyor systems engineered by NCC Automated Systems. Built specifically for food processing and pet food manufacturing, our conveyor solutions move dry kibble, raw ingredients, packaged treats, and delicate food products efficiently through your facility.
From raw material handling and washdown sanitary transfers to high-speed end-of-line packaging lines, NCC designs, builds, and integrates tailored conveyance systems that eliminate bottlenecks, ensure gentle product handling, and withstand harsh sanitation environments.
🐕🥩 Key Features & Capabilities:
Sanitary & Washdown Engineering: Stainless steel construction designed for complete cleanability, meeting strict FSMA and USDA sanitary standards.
Specialized Product Transport: Custom belting and transfer designs specifically engineered for wet, oily, abrasive, or delicate food and pet food materials.
Flexible Systems Integration: Easily connects food extruders, fryers, ovens, scales, baggers, and case packers into one continuous flow.
Custom Layout Configurations: Incline, decline, curve, and overhead conveyor routing optimized to maximize your facility’s floor space.
Reduced Maintenance Downtime: Tool-less belt removal and open-frame geometries facilitate rapid cleaning and quick maintenance.
📈 Scale your food or pet food processing line with custom conveyor automation engineered for durability and hygiene.
👉 Request a Custom System Design or Quote: https://www.nccas.com/contact/
#NCCAutomatedSystems #FoodProcessing #PetFoodManufacturing #SanitaryConveyors #PackagingAutomation #ConveyorSystems #MaterialHandling #FoodSafety #CustomEngineering