NCC Automated Systems Successfully Completes FAT for Large-Scale Conveyor & Material Handling Solution Serving Leading Pet Food Manufacturer
Innovative conveyor network demonstrates how customized material handling solutions can maximize throughput, optimize space utilization, and support future growth.
Souderton, PA – NCC Automated Systems, a leader in custom conveyor and material handling solutions, has released a new video showcasing a large-scale conveyor automation project designed for one of North America’s leading consumer packaged goods manufacturers.
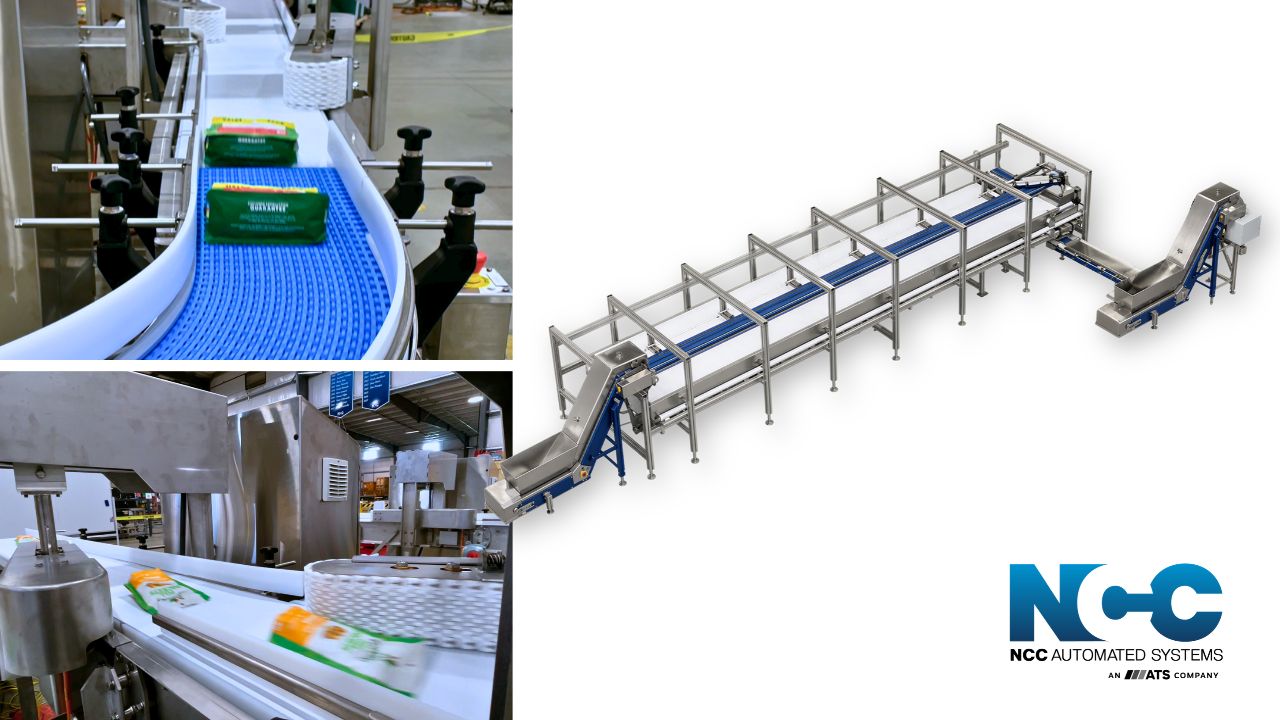
The installation demonstrates NCC’s ability to engineer highly customized conveyor systems that support complex production environments, efficiently moving products between multiple processing, packaging, storage, and distribution areas while maximizing facility throughput.
The project features an extensive network of conveyors and material handling equipment designed to transport products seamlessly throughout the facility. By strategically integrating accumulation, routing, elevation changes, and product flow management, the system helps improve operational efficiency while reducing manual handling requirements.
“Every facility presents unique challenges when it comes to product flow, available space, production rates, and future expansion plans,” said Jesse Blazek, Director Sales & Applications at NCC Automated Systems. “Our team works closely with customers to design conveyor and material handling systems that fit their operation, not the other way around. This project is a great example of how custom automation can help manufacturers improve productivity while creating a scalable foundation for future growth.”
Unlike standardized conveyor offerings, NCC specializes in developing tailored solutions that address specific operational goals and facility constraints. From compact conveyor sections and accumulation systems to facility-wide material handling networks, NCC engineers each solution to support long-term performance and reliability.
The featured installation highlights several key advantages manufacturers seek when investing in conveyor automation:
- Increased production throughput
- Improved product flow and line efficiency
- Reduced manual product handling
- Better utilization of available floor space
- Enhanced workplace safety
- Scalable infrastructure for future expansion
- Reliable movement of products between multiple operational areas
As manufacturers continue to face labor challenges, increasing production demands, and facility space limitations, customized conveyor automation has become a critical component of efficient plant operations.
Whether supporting packaging lines, processing operations, warehouse distribution, pallet handling, or end-of-line packaging applications, NCC Automated Systems designs and manufactures conveyor solutions that help manufacturers move products smarter, faster, and more efficiently.
Watch the Video
See how NCC Automated Systems engineered a customized conveyor and material handling solution to optimize product flow and support high-volume manufacturing operations. – https://www.nccas.com/youtube-video/custom-conveyor-systems-for-food-and-pet-food-manufacturers/
About NCC Automated Systems
NCC Automated Systems designs and manufactures custom conveyor systems, material handling solutions, accumulation systems, storage and distribution conveyors, and integrated automation solutions for manufacturers across a wide range of industries. With a focus on engineering innovation, reliability, and customer-specific solutions, NCC helps companies improve efficiency and maximize operational performance throughout their facilities.
Learn more at: www.nccas.com